From sludge generation to technology selection and resource recovery — everything environmental engineers and plant managers need to make informed decisions.

Every industrial facility that treats wastewater eventually encounters the same challenge — sludge.
Whatever you’re operating — pharmaceutical, textile, paper, food, chemical, or municipal WWTP — wastewater treatment doesn’t eliminate contaminants. It concentrates them into a semi-solid by-product known as sludge, which needs to be managed.
But for many industries, this part receives attention only after it starts causing issues:
- Unexpected rise in disposal costs
- Insufficient storage areas
- Equipment struggling to achieve the desired moisture content
- Stringent environmental regulations
By then, sludge has already become one of the largest recurring operating expenses within the wastewater treatment system.
However, it’s also an opportunity in disguise. When managed correctly, sludge is no longer just a waste product awaiting disposal.
This is a detailed guide on every stage of industrial sludge management — from sludge generation to appropriate treatment technologies to reducing lifecycle costs. Whether you are an environmental engineer, EHS manager, plant manager, consultant, or wastewater professional, this guide will help you make informed decisions that improve operational performance while ensuring environmental compliance.
What Is Industrial Sludge?
Industrial sludge is the semi-solid residue produced during industrial wastewater treatment after contaminants are separated from water.
During wastewater treatment, pollutants are removed from the liquid stream. Rather than disappearing, these contaminants become concentrated into sludge. Depending on the industry, sludge may contain:
| Sludge Component | Typical Relevance |
|---|---|
| Suspended solids | Settleable particles separated during treatment |
| Organic matter | Biodegradable material from process wastewater |
| Biological solids | Microbial biomass generated in biological treatment |
| Treatment chemicals | Coagulants, flocculants, lime, alum, or ferric salts |
| Oils and grease | Floatable or emulsified contaminants from industrial processes |
| Heavy metals | Metals that may affect hazard classification and disposal route |
| Nutrients | Nitrogen, phosphorus, and other recoverable compounds |
| Fine particulate matter | Small particles that influence filterability and dewatering performance |
| Microorganisms | Living or inactive biological organisms present in sludge |
| Inorganic compounds | Minerals, salts, and non-biodegradable residues |
Fresh sludge typically contains between 70% and 99% water, making it bulky, heavy, unstable, and expensive to transport. For this reason, the primary objective of sludge management is not simply disposal — but reducing water content to ensure environmentally responsible treatment.
Modern sludge management focuses on reducing transportation costs, improving operational efficiency, recovering valuable resources, minimizing environmental impact, and supporting circular economy initiatives. Today, industries are increasingly moving away from simply disposing of sludge and towards integrated strategies that combine characterization, thickening, dewatering, drying, stabilization, and resource recovery.
Why Does Every Wastewater Treatment Plant Produce Sludge?
A common misconception is that sludge is only generated in municipal sewage treatment plants. In reality, every wastewater treatment system generates sludge because contaminants removed from wastewater must accumulate somewhere.
The cleaner the treated water becomes, the greater the quantity of solids removed. Those solids become sludge.
Industries generating sludge include textile manufacturing, pharmaceutical production, chemical industries, food processing, dairy plants, breweries, beverage manufacturing, paper and pulp mills, electroplating, automobile manufacturing, and municipal wastewater treatment.
Regardless of industry, sludge management should be viewed as an essential component of wastewater treatment — not as a separate downstream activity.
Industrial Sludge vs Wastewater
Although the two terms are often used interchangeably, wastewater and sludge are fundamentally different materials.
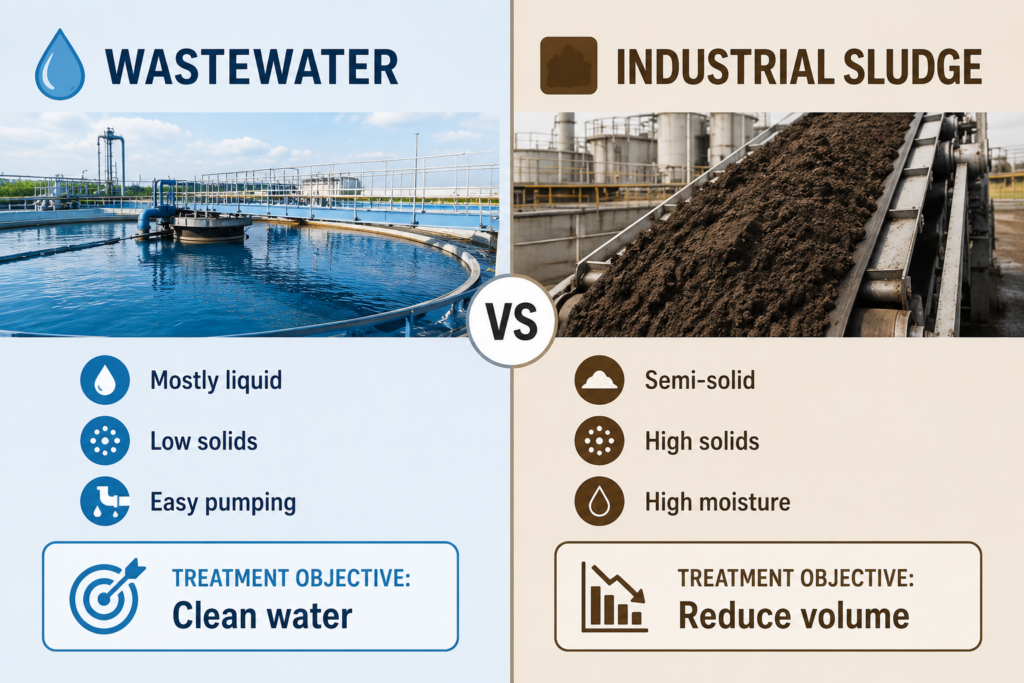
A useful analogy is coffee brewing. The coffee maker separates liquid coffee from the coffee grounds. Wastewater treatment works in much the same way — clean water leaves the process while concentrated contaminants remain behind as sludge.
How Industrial Sludge Is Generated
Industrial sludge is generated throughout several stages of wastewater treatment. Understanding where sludge originates is important because each stage produces sludge with different physical and chemical properties.
1. Preliminary Treatment
Large debris such as plastics, rags, grit, sand, and floating materials are removed to protect downstream equipment. Although relatively little sludge is generated at this stage, these screenings require separate disposal.
2. Primary Treatment
Wastewater enters sedimentation tanks where heavier suspended solids settle naturally under gravity. These settled solids form primary sludge, which usually contains suspended solids, organic material, food particles, fibres, sediments, and oils and grease. Because it consists of larger particles, primary sludge generally dewaters more easily than biological sludge.
3. Secondary (Biological) Treatment
After primary treatment, dissolved organic pollutants remain in the wastewater. These are removed by microorganisms through biological treatment processes such as the Activated Sludge Process (ASP), Sequencing Batch Reactors (SBR), Moving Bed Biofilm Reactors (MBBR), or Membrane Bioreactors (MBR).
As microorganisms consume pollutants, they multiply rapidly. Excess microbial biomass must then be removed from the system — this forms secondary sludge, also called waste activated sludge (WAS). Secondary sludge contains much finer particles and significantly more bound water than primary sludge, making it more difficult to dewater.
4. Chemical Treatment
Many industrial wastewater treatment plants add chemicals such as alum, ferric chloride, lime, and polymers. These chemicals react with dissolved contaminants to form solid particles that settle out as chemical sludge. The properties of chemical sludge vary significantly depending on the treatment chemicals used and the wastewater composition.
Types of Industrial Sludge
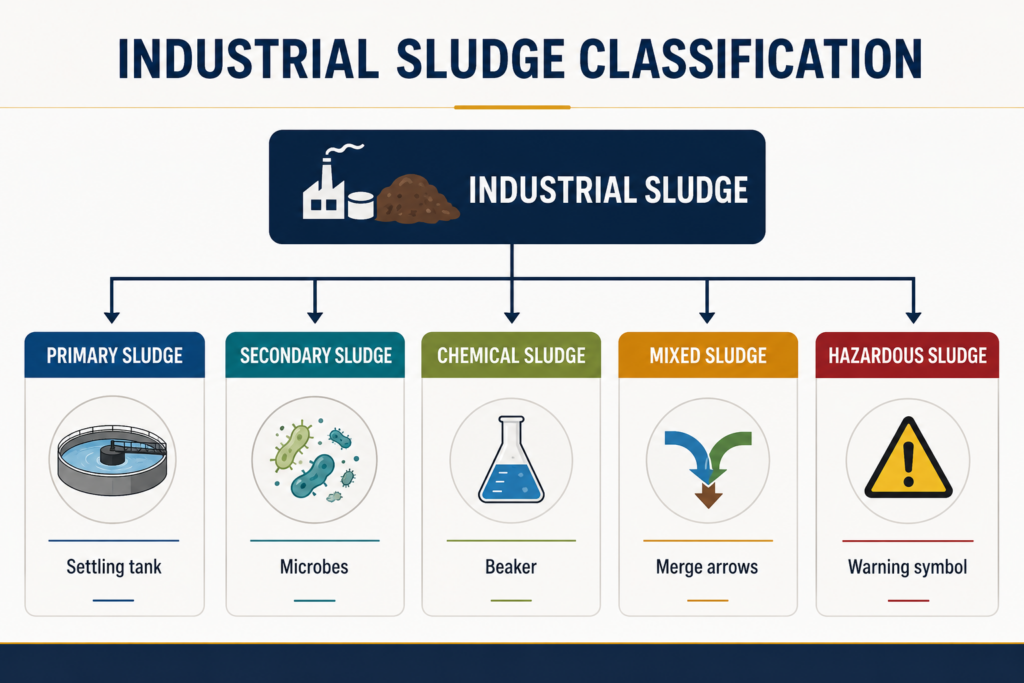
Selecting an appropriate sludge management system begins with understanding the type of sludge being treated.
1. Primary Sludge
High settleability, larger particle size, easier dewatering, higher suspended solids, lower biological activity. Common in food industries, municipal plants, dairy processing, and paper mills.
2. Secondary Sludge
High moisture content, fine particles, difficult to dewater, compressible structure, high organic content. Generally requires more conditioning before mechanical dewatering.
3. Chemical Sludge
Produced through chemical precipitation — may contain lime, alum, ferric salts, metal hydroxides, or chemical precipitates. Behaviour depends heavily on the chemicals used.
4. Mixed Sludge
Many facilities combine primary and secondary sludge. Although this simplifies operation, mixed sludge behaves differently from either sludge individually.
5. Hazardous Sludge
Industries such as electroplating, pharmaceuticals, battery manufacturing, and specialty chemicals may generate hazardous sludge containing heavy metals or toxic compounds, requiring specialized handling and disposal.
Why Sludge Characteristics Matter
One of the biggest mistakes industries make is assuming that all sludge behaves similarly. It doesn’t.
Two sludge samples may both contain 80% moisture, yet one dewaters efficiently while the other remains extremely difficult to process. The difference lies in sludge characteristics. Key parameters include moisture content, dry solids concentration, organic matter, particle size, filterability, density, bound water, free water, oil and grease, heavy metal concentration, and hazard classification.
Understanding these properties allows engineers to design treatment systems that achieve the desired performance without unnecessary operating costs.
Sludge quantity alone should never determine equipment selection. Two facilities producing the same daily sludge volume may require completely different treatment technologies because sludge behaviour depends on composition — not just volume.
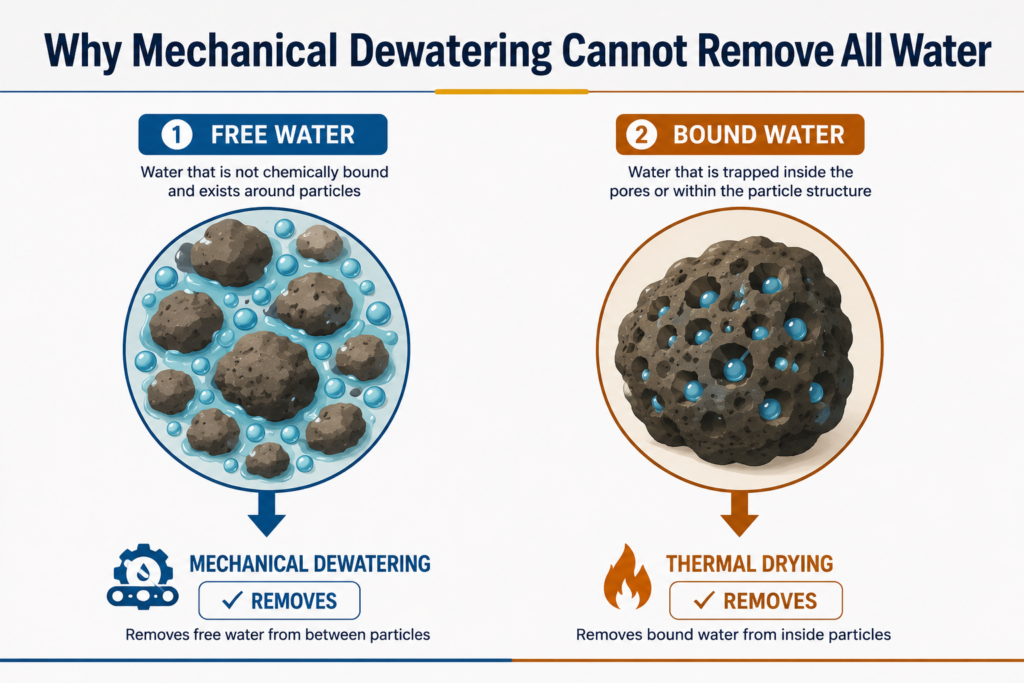
Expecting a filter press or screw press to produce completely dry sludge often leads to disappointment. Mechanical dewatering and thermal drying perform different functions and should not be viewed as competing technologies.
The Industrial Sludge Management Process
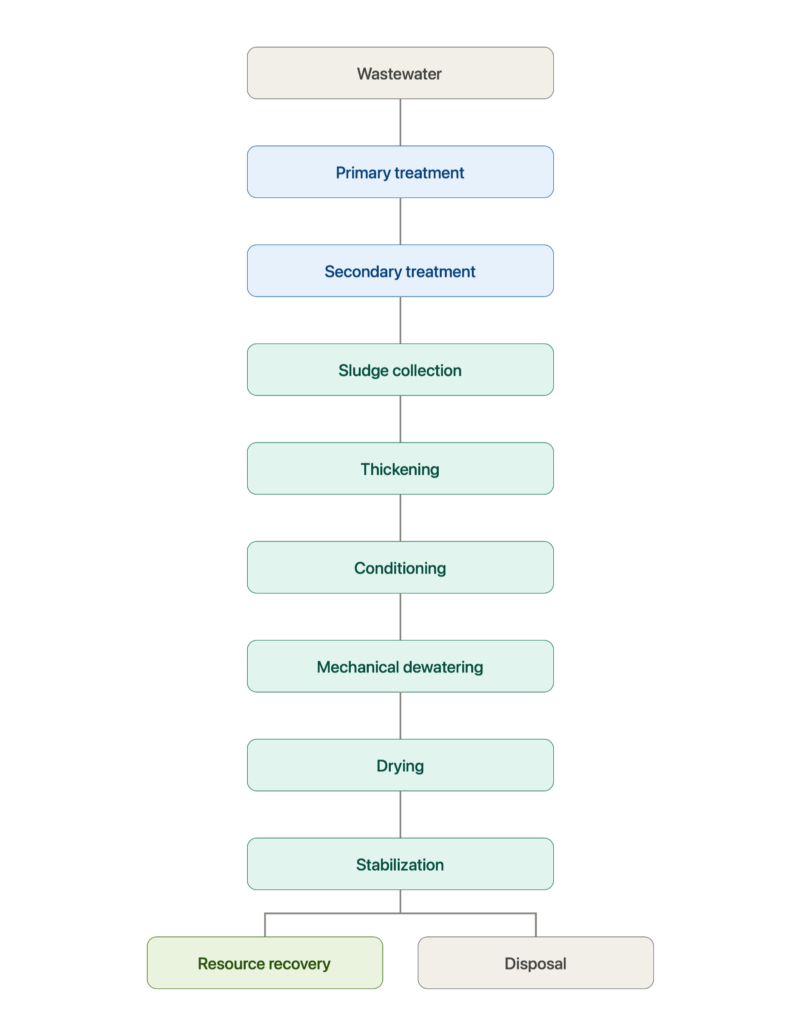
Effective sludge management is not a single operation — it is a carefully designed sequence of processes that progressively reduce sludge volume, improve handling characteristics, lower disposal costs, and maximize opportunities for resource recovery.
Each stage prepares the sludge for the next. When one stage is poorly designed or skipped, downstream equipment becomes less efficient, operating costs increase, and disposal challenges multiply.
Wastewater → Collection → Thickening → Conditioning → Dewatering → Drying → Stabilization → Recovery or Disposal
The objective is not simply to produce “dry sludge.” The objective is to achieve the lowest lifecycle cost while meeting operational and environmental requirements.
Step 1: Sludge Thickening
The first stage after sludge collection is usually thickening. Thickening removes a portion of the water before mechanical dewatering. Although it does not produce a dry sludge cake, it significantly reduces the volume that must be processed downstream.
Think of thickening as concentrating sludge rather than drying it. Less volume means smaller pumps, reduced polymer consumption, lower energy use, and improved downstream performance.
Objectives of thickening: reduce sludge volume, increase solids concentration, reduce pumping costs, improve dewatering efficiency, reduce downstream equipment size, and lower operating costs.
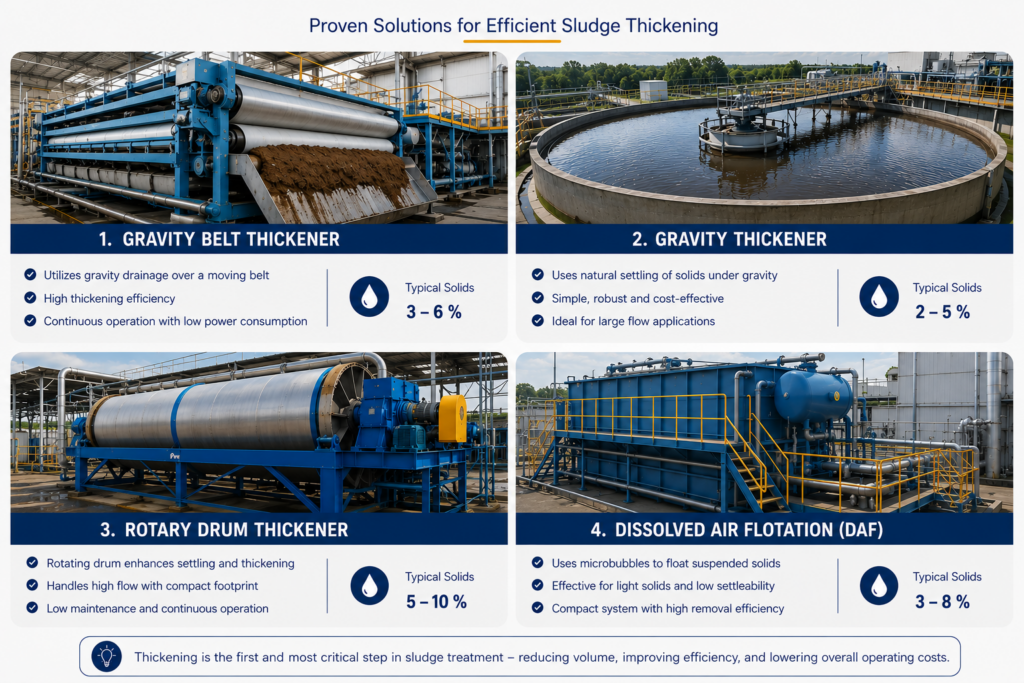
a. Gravity Thickener
Relies on the natural settling of solids. Best suited for primary sludge and high-settleability sludge. Advantages: simple operation, low energy consumption, low maintenance. Limitations: large footprint, less effective for biological sludge.
b. Gravity Belt Thickener
A porous moving belt allows water to drain while solids remain on the belt. Suitable for biological and mixed sludge, with continuous operation and relatively low energy consumption.
c. Rotary Drum Thickener
A rotating perforated drum separates water while retaining solids. Often selected where space is limited, continuous operation is required, or moderate sludge quantities are generated.
d. Dissolved Air Flotation (DAF)
Instead of allowing solids to settle, DAF uses microscopic air bubbles to float lighter solids to the surface — frequently used where sludge has poor settling characteristics.
Thickening is sometimes overlooked because it appears to provide only modest moisture reduction. However, even a small increase in solids concentration before dewatering can significantly reduce polymer consumption and energy costs throughout the remainder of the treatment process.
Step 2: Sludge Conditioning
Before mechanical dewatering, sludge often requires conditioning. Conditioning changes the physical properties of sludge, allowing water to separate more easily during dewatering.
Without proper conditioning, filter media clog more quickly, polymer consumption increases, cake solids decrease, equipment capacity falls, and energy costs rise.
a. Chemical Conditioning
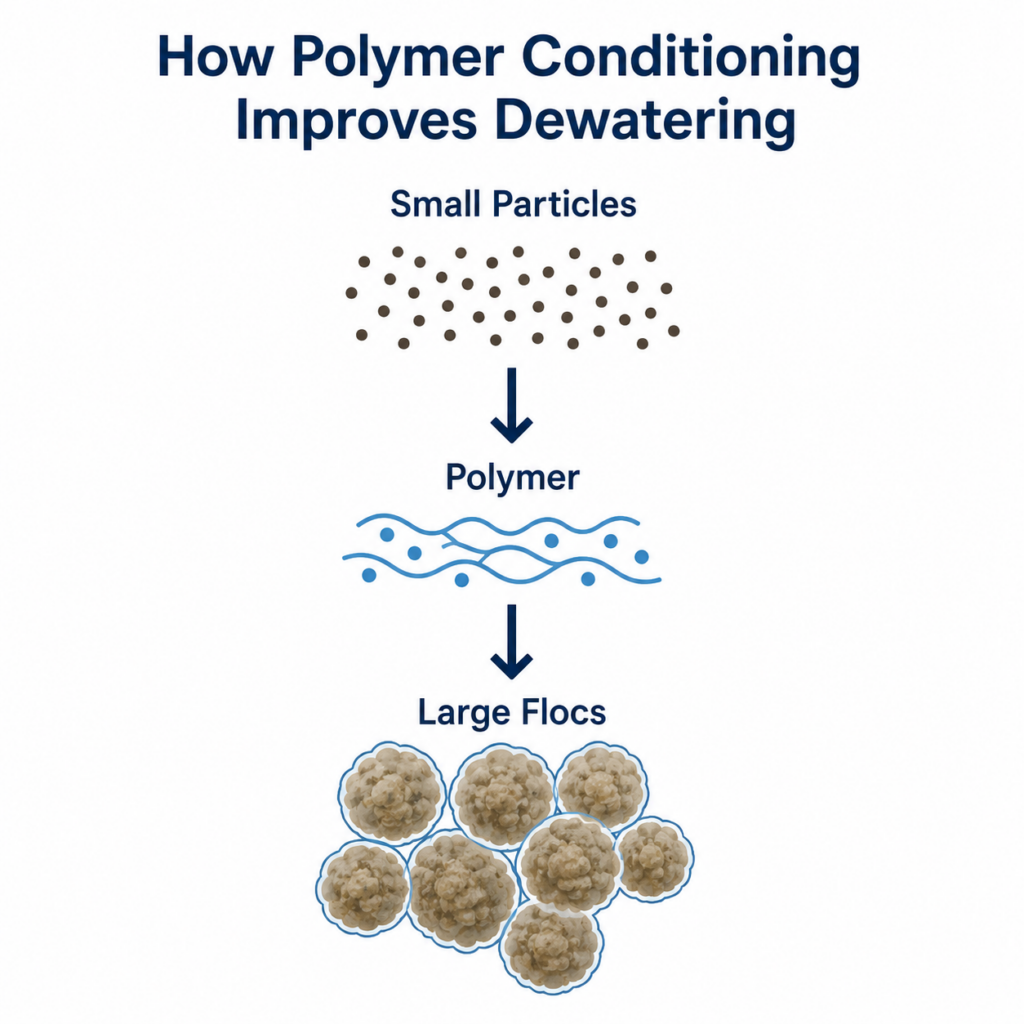
The most common approach, using cationic polymers, ferric chloride, alum, or lime. These chemicals help small sludge particles combine into larger flocs that release water more easily.
b. Thermal Conditioning
Heat changes the structure of sludge particles and improves water release. Although more energy intensive, thermal conditioning may be appropriate for certain industrial sludges.
c. Biological Conditioning
Some biological treatment methods improve sludge stability and dewatering characteristics before further processing.
Many plants attempt to compensate for poor sludge characteristics by increasing polymer dosage. In reality, excessive polymer use often increases operating costs without significantly improving cake dryness. Proper sludge characterization and polymer optimization generally produce better long-term results.
Step 3: Mechanical Dewatering
After thickening and conditioning, sludge still contains a large amount of water. The purpose of mechanical dewatering is to remove as much free water as possible and produce a sludge cake that can be transported, stored, or further processed.
How to Choose the Right Dewatering Technology
Many facilities choose equipment based on what neighbouring plants use, lowest purchase price, or vendor recommendations. Unfortunately, these are rarely the right criteria. Instead, technology selection should begin with the sludge itself. Ask: What type of sludge is being treated? What cake solids are required? How much space is available? What is the disposal route? How much labour is available? What is the energy budget?
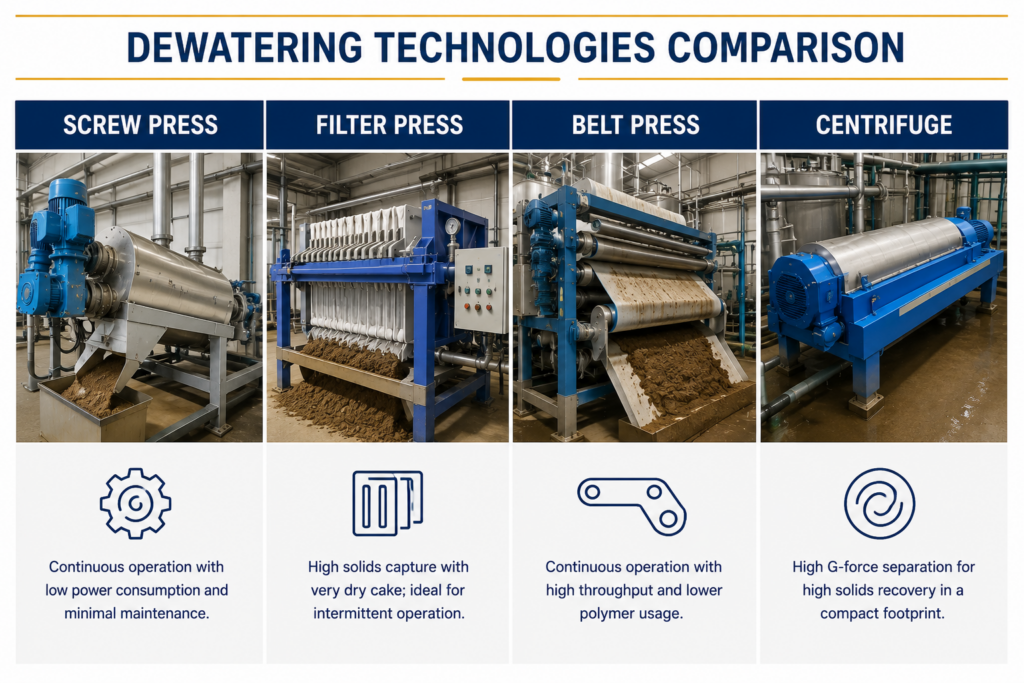
a. Screw Press
Gradually compresses sludge using a slowly rotating screw inside a cylindrical screen. Water drains through the screen while solids become progressively compressed. Advantages: low energy consumption, continuous operation, compact footprint, low maintenance, quiet operation, good for biological sludge. Limitations: cake dryness depends heavily on sludge characteristics; not suitable for every sludge type. Best suited for: municipal, biological, food industry, and mixed sludge.
b. Filter Press
Uses hydraulic pressure to squeeze water from sludge trapped between filter plates — generally producing one of the driest mechanically dewatered sludge cakes. Advantages: high cake solids, excellent water removal, suitable for difficult industrial sludges. Limitations: batch operation, longer cycle times, higher labour requirements. Best suited for: chemical sludge, mining sludge, metal finishing, and sludge requiring high cake dryness.
c. Belt Filter Press
Compresses sludge between moving belts while water drains away. Advantages: continuous operation, moderate energy consumption, high throughput. Limitations: requires careful polymer optimization, larger installation footprint.
d. Centrifuge
Separates solids using centrifugal force rather than pressure. Advantages: highly automated, compact, high throughput. Limitations: higher energy use, greater maintenance, wear caused by abrasive sludge.
Engineer’s Decision Framework
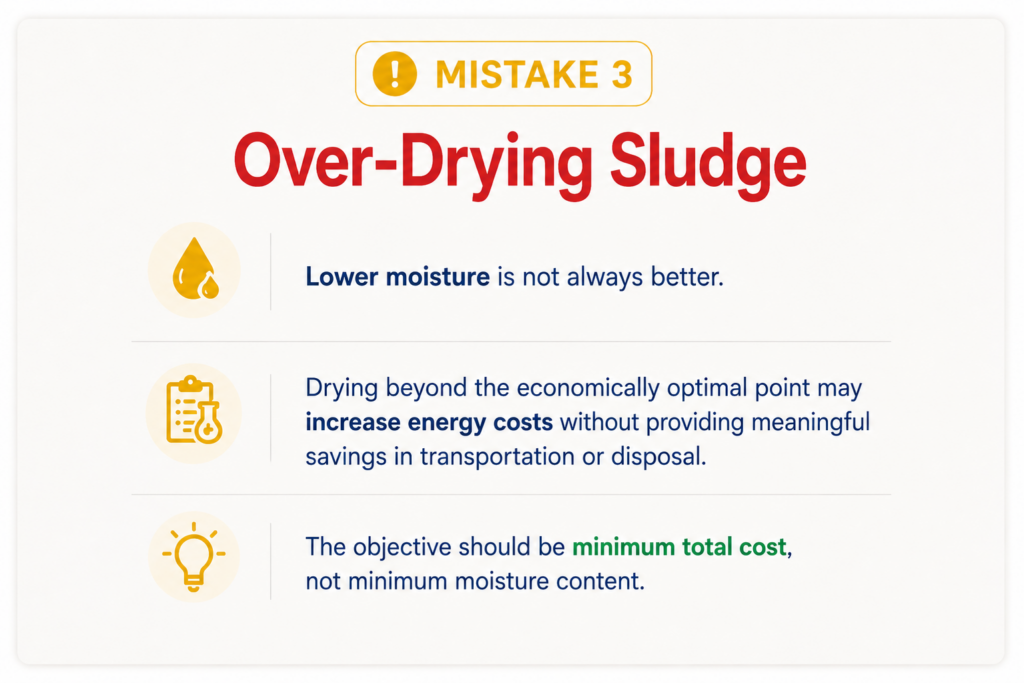
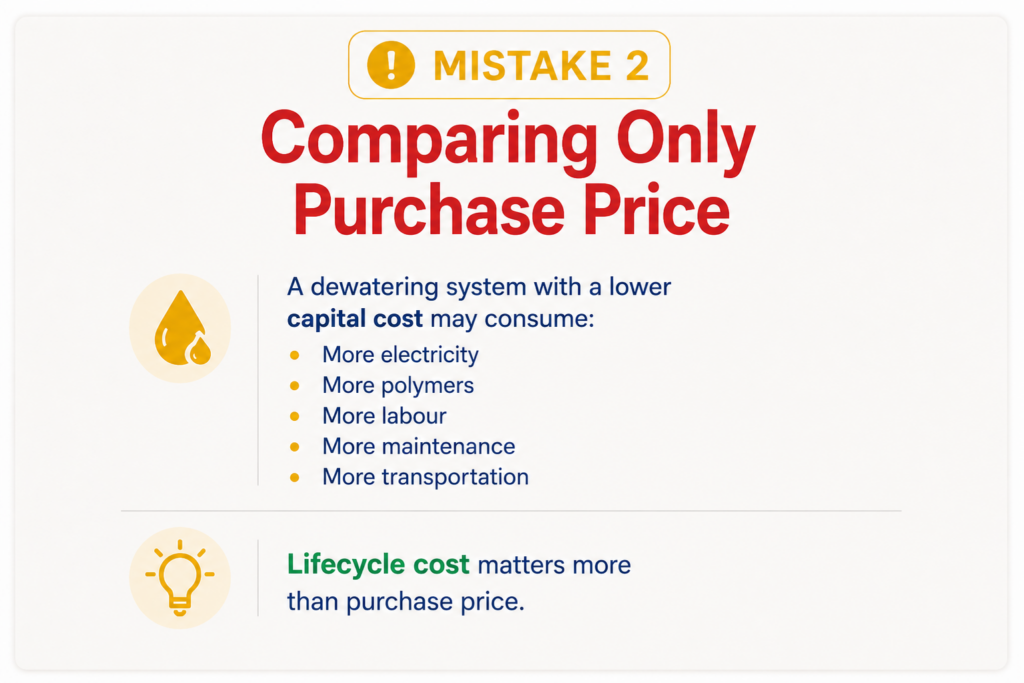
Instead of asking “Which machine is the best?” ask: “Which machine minimizes my total sludge management cost?” That answer depends on polymer usage, labour, electricity, maintenance, cake dryness, transportation, disposal charges, and future expansion. The equipment with the lowest purchase price rarely has the lowest lifecycle cost.
Lifecycle Cost vs Capital Cost
Imagine two dewatering systems. System A has a lower purchase price but higher energy use, higher polymer use, and lower cake solids. System B has a higher purchase price but lower operating costs, better cake dryness, and lower disposal cost. System A may appear cheaper during procurement but cost significantly more over the next ten years. Successful sludge management decisions evaluate Total Cost of Ownership (TCO) rather than equipment price alone.
Step 4: Sludge Drying
Mechanical dewatering removes only free water. Bound water remains trapped inside sludge particles.
For facilities where disposal costs are high, sludge drying often provides the greatest long-term savings. Drying removes additional moisture using solar energy, thermal energy, or waste heat — resulting in lower weight, smaller volume, improved storage, reduced odour, higher calorific value, and lower transportation costs.
Solar Drying vs Thermal Drying
This is one of the most common questions in sludge management. The answer is simple: neither technology is universally better. The correct choice depends on project requirements.
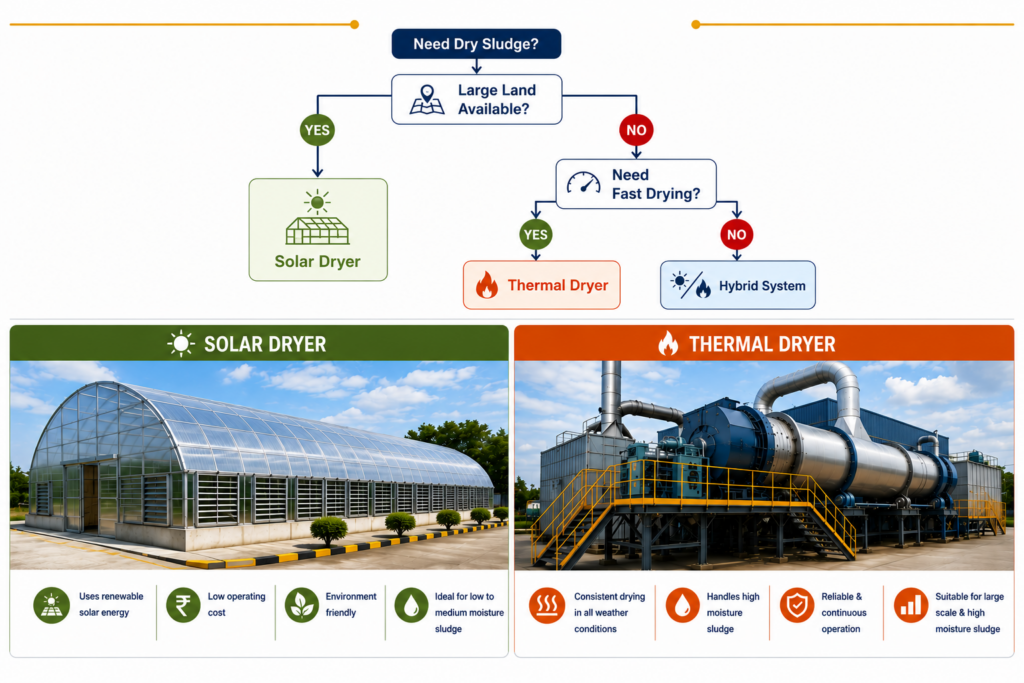
| Decision Factor | Solar Drying | Thermal Drying |
|---|---|---|
| Land Requirement | High | Low |
| Energy Requirement | Very Low | High |
| Drying Speed | Slow | Fast |
| Weather Dependency | Yes | No |
| Automation | Moderate | High |
| Throughput | Medium | High |
| Operating Cost | Low | Higher |
Engineer’s Technology Selection Checklist
Before selecting any drying technology, ask: What is the annual sludge quantity? Is land available? What is the local climate? Are energy costs high? What moisture content is actually required? Can waste heat be recovered? What is the disposal route? Will sludge production increase in the future?
Cost Reduction Pyramid
One of the easiest ways to understand sludge management is to think of it as a pyramid. The greatest savings are rarely achieved through a single piece of equipment. Instead, costs are progressively reduced through: sludge characterization, thickening, conditioning, mechanical dewatering, drying, resource recovery, and optimized disposal. Each stage reduces the cost burden passed to the next.
The most successful sludge management projects are not those that produce the driest sludge — they are the ones that achieve the lowest total lifecycle cost while meeting environmental and operational requirements.
Step 5: Sludge Stabilization
Fresh sludge is biologically active. If left untreated, it continues to decompose, generating odours, attracting pests, producing greenhouse gases, and creating handling challenges. Sludge stabilization reduces biological activity, making sludge safer to store, transport, and process.
a. Biological Stabilization
Aerobic digestion suits smaller plants, reduces odour, and requires continuous aeration. Anaerobic digestion suits medium and large facilities, produces biogas for energy generation, reduces sludge volume, and improves sustainability.
b. Chemical Stabilization
Chemical additives such as lime increase pH, reducing pathogen activity and slowing biological decomposition — suitable where pathogen reduction or agricultural reuse is being considered (subject to regulations).
c. Thermal Stabilization
Heat destroys pathogens while improving sludge stability, often integrated with thermal drying systems in larger industrial facilities.
Sludge Disposal and Resource Recovery
Historically, sludge management ended with disposal. Today, the objective is shifting from “dispose of sludge” to “recover value from sludge wherever feasible.” The best disposal strategy depends on sludge composition, moisture content, hazard classification, local regulations, transportation costs, available infrastructure, and sustainability objectives.
a. Landfill Disposal
Remains one of the most common disposal routes, but is becoming increasingly expensive due to rising landfill charges, transportation costs, environmental regulations, and limited landfill capacity.
b. Co-processing in Cement Kilns
Certain industrial sludges can be used as alternative fuel or raw material in cement manufacturing, offering reduced landfill dependence, energy recovery, lower fossil fuel consumption, and better resource utilization — subject to moisture content, calorific value, heavy metal concentration, chloride content, and regulatory approval.
c. Composting
Organic sludge with low contamination levels may be composted under controlled conditions, requiring proper carbon-to-nitrogen ratio, controlled moisture, aeration, temperature monitoring, and pathogen reduction. Generally unsuitable for hazardous industrial sludge.
d. Energy Recovery
Industries increasingly view sludge as a renewable energy source — biogas production, refuse-derived fuel (RDF), alternative fuels, and waste-to-energy systems can offset operational costs while reducing landfill dependence.
e. Resource Recovery and Circular Economy
Modern sludge management extends beyond waste reduction. Industries increasingly recover phosphorus, nitrogen, organic matter, energy, and in some systems, process water. Instead of asking “How do we dispose of sludge?”, forward-thinking organizations ask “How much value can we recover before disposal becomes necessary?”
Common Mistakes Industries Make
After working with numerous wastewater treatment systems, one observation remains consistent: most sludge management problems are not caused by poor equipment. They are caused by poor planning.
The Technology Selection Framework
Before investing in any sludge management solution, answer these five questions.
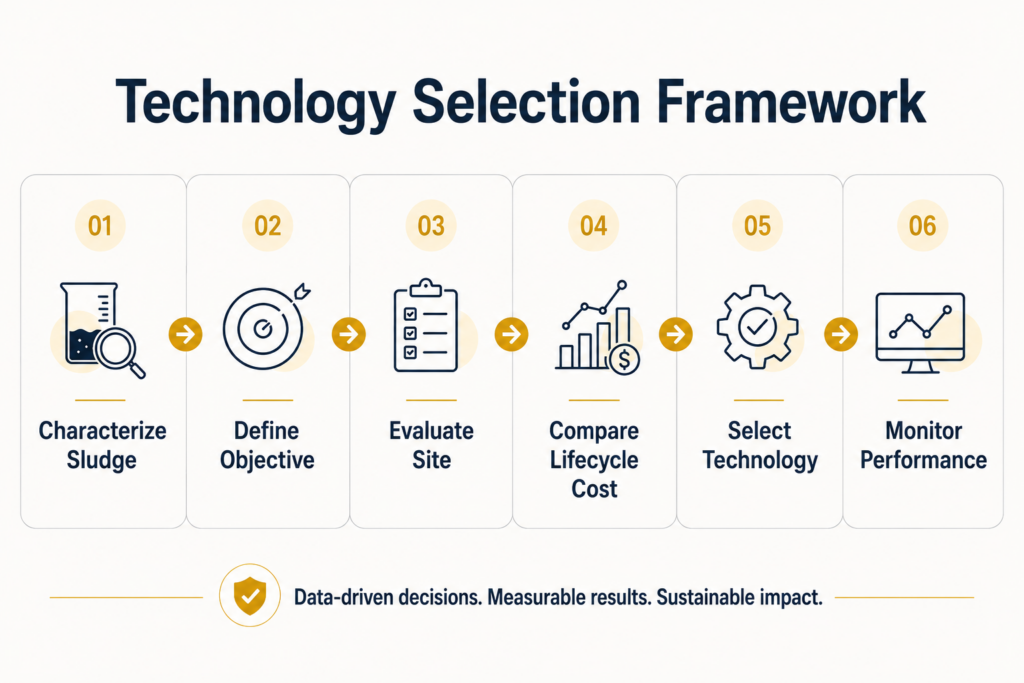
Step 1 — Understand Your Sludge
Determine sludge type, moisture content, dry solids, hazard classification, organic content, and particle size. Without proper characterization, technology selection becomes guesswork.
Step 2 — Define Your Objective
What is your primary goal — lower disposal costs, reduced transport frequency, producing fuel, recovering resources, or meeting regulatory requirements? Different objectives require different technologies.
Step 3 — Evaluate Site Constraints
Consider land availability, utilities, climate, labour, energy costs, and future capacity. These constraints often influence technology selection as much as sludge characteristics.
Step 4 — Compare Lifecycle Costs
Evaluate capital expenditure, operating expenditure, polymer consumption, energy, labour, maintenance, disposal savings, and ROI. Never compare equipment based solely on purchase price.
Step 5 — Think Beyond Disposal
Ask whether your sludge can become compost, alternative fuel, biogas, recovered nutrients, or industrial raw material. This mindset transforms sludge management from a cost centre into a value recovery opportunity.
Future Trends in Industrial Sludge Management
Industrial sludge management is evolving rapidly. Several emerging technologies are reshaping how industries approach treatment, monitoring, and resource recovery.
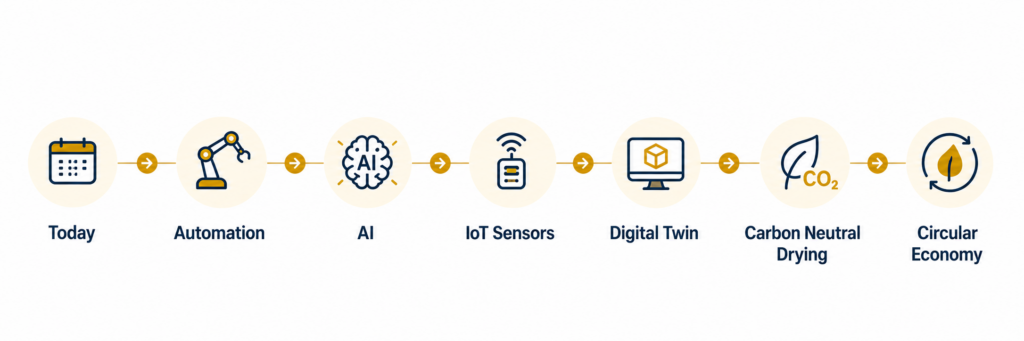
1. AI-Powered Process Optimization
Artificial intelligence is beginning to optimize polymer dosing, monitor sludge characteristics in real time, predict equipment performance, and improve process efficiency through data-driven decision-making.
2. Digital Twins
Digital twin technology enables operators to simulate sludge treatment processes before implementing operational changes, reducing risk and improving system performance.
3. Smart Sensors and IoT
Modern systems increasingly incorporate sensors that monitor solids concentration, moisture content, flow rates, equipment health, and energy consumption — enabling predictive maintenance and improved process control.
4. Waste Heat Recovery
Rather than generating new thermal energy, industries are increasingly using waste heat from boilers, engines, and industrial processes for sludge drying, reducing operating costs and carbon emissions.
5. Carbon Reduction
Lower energy consumption, renewable energy integration, and efficient sludge drying technologies are becoming central to industrial decarbonization strategies.
6. Phosphorus Recovery
As phosphorus becomes a strategically important resource, technologies capable of recovering phosphorus from sludge are gaining attention worldwide.
7. PFAS and Emerging Contaminants
Persistent contaminants such as PFAS are creating new challenges for sludge treatment and disposal, requiring advanced treatment strategies and closer regulatory oversight.
8. Circular Economy Integration
Rather than viewing sludge as waste, industries increasingly consider it a source of energy, nutrients, reusable materials, and alternative fuels.
Key Takeaways
- Sludge management begins with understanding sludge characteristics — not equipment selection.
- Thickening, conditioning, dewatering, drying, and stabilization each play a distinct role in reducing lifecycle costs.
- There is no universally “best” sludge treatment technology; the right solution depends on sludge composition, operational goals, and site constraints.
- Lifecycle cost should guide investment decisions rather than capital cost alone.
- Modern sludge management is shifting from disposal toward resource recovery and circular economy principles.
Frequently Asked Questions
What is industrial sludge?
Industrial sludge is the semi-solid residue generated during industrial wastewater treatment after contaminants are removed from wastewater.
Why does sludge contain so much water?
Most sludge contains a high proportion of free and bound water, making it bulky and heavy until treated.
What is the difference between primary and secondary sludge?
Primary sludge settles during sedimentation, while secondary sludge consists mainly of biological solids generated during biological treatment.
Why is secondary sludge harder to dewater?
It contains finer particles and more bound water than primary sludge.
What is sludge thickening?
A process that increases solids concentration by removing part of the water before dewatering.
What is sludge conditioning?
A treatment step that improves water release before mechanical dewatering.
What is sludge dewatering?
Mechanical removal of free water to produce a transportable sludge cake.
Is dewatering the same as drying?
No. Dewatering removes mainly free water, while drying removes additional bound water using heat or solar energy.
Which dewatering technology is best?
The answer depends on sludge characteristics, operating costs, and treatment objectives.
What is sludge cake?
The semi-solid material produced after mechanical dewatering.
What is sludge stabilization?
The process of reducing biological activity, odours, and pathogens before disposal or reuse.
Can sludge be composted?
Some organic sludges can, provided they meet regulatory and quality requirements.
Can sludge be used as fuel?
Certain dried sludges may be suitable for energy recovery or co-processing.
Why is sludge characterization important?
It ensures the selected treatment technology matches sludge behaviour and performance requirements.
What is bound water vs free water?
Bound water is trapped within sludge particles and cannot be removed by mechanical dewatering alone; free water can be removed through thickening or mechanical dewatering.
Is lower moisture always better?
No. The optimum moisture depends on the intended disposal or reuse route.
How can industries reduce sludge disposal costs?
By combining sludge characterization, optimized thickening, efficient dewatering, appropriate drying, and resource recovery.
What is hazardous sludge?
Sludge containing substances that require specialized handling and disposal due to environmental or health risks.
What are the latest trends in sludge management?
AI-assisted optimization, digital twins, IoT monitoring, waste heat recovery, PFAS management, and circular economy approaches.
How do I choose the right sludge management system?
Begin with sludge characterization, define your objectives, assess site constraints, compare lifecycle costs, and evaluate opportunities for resource recovery.
Summing It Up
Industrial sludge management is no longer simply about disposing of a waste stream. It is a strategic engineering function that directly influences operating costs, environmental performance, regulatory compliance, and long-term sustainability.
Facilities that understand their sludge, select technologies based on engineering data rather than assumptions, and evaluate projects using lifecycle costs instead of capital costs consistently achieve better operational outcomes.
As environmental regulations tighten and resource recovery becomes increasingly important, sludge management will continue to evolve from a disposal challenge into an opportunity for operational optimization and value creation.
Need Help Optimizing Your Sludge Management System?
Selecting the right sludge treatment solution requires more than comparing equipment specifications. Sludge characteristics, treatment objectives, operating costs, site constraints, regulatory requirements, and long-term scalability all influence the best solution. Thermarex specializes in designing integrated sludge management solutions, including thickening, dewatering, drying, and resource recovery systems tailored to industrial applications.
Talk to a Thermarex Engineer